Separate the CNC system, data and spindle-power boundary; do not promise that any outage avoids tool damage. Plan the project from the CNC manufacturer power requirements and supported control shutdown behavior.
Section 01
Split Control and Main Power
Can a small UPS keep a CNC machine cutting? For Machine tool managers and CNC integrators, the answer must stay inside the project boundary: Not as a general solution. Separate the CNC control, data and communication scope from spindle and axis drives. Continued motion requires the machine manufacturer's approved design. A control backup should not be marketed as whole-machine power continuity. The next step is boundary map: CNC / data / axes / spindle / auxiliaries, using CNC manufacturer power requirements and supported control shutdown behavior.
Start by drawing the boundary on the machine itself. List the control cabinet, the data path, the axis drives, the spindle and the auxiliaries. Then mark which items have to stay powered for the sequence you want. Spindle and axes usually stay off the small backup. Coolant pumps, chip conveyors and hydraulic units stay on the plant feed for the same reason.
A boundary map keeps the split visible. Fill it with the machine you actually have, not a generic CNC.
When the supply drops, the controller gets the seconds it needs. The spindle coasts. Keeping those two boundaries separate keeps the proposal honest, because the UPS protects only the control service.
| Decision area | Project question | Required output |
|---|---|---|
| Split Control and Main Power | Can a small UPS keep a CNC machine cutting? | Boundary map: CNC / data / axes / spindle / auxiliaries |
| Define the Supported Benefit | What can control backup help accomplish? | Benefit table: function / supported action / input / limitation |
| Use Manufacturer Requirements | Which power requirements should guide selection? | Interface schedule: input / waveform / transition / approved source |
Section 02
Define the Supported Benefit
The next step is to say what the backup actually does. A control backup supports the machine's specified state-saving, communication or controlled-stop behavior where the interface permits it. Describe that function precisely. It does not prevent every workpiece defect, tool collision or other mechanical consequence of supply loss.
Write each candidate benefit as a function with an action, the input it needs and its limit.
Stating the benefit this way prevents two common mistakes. The first is overselling: a team says the UPS prevents scrapped parts, then a collision happens and the equipment takes the blame. The second is underselling: nobody writes down what the save needs, so the battery interval gets guessed. Both problems disappear when the function, action, input and limit sit on one line.
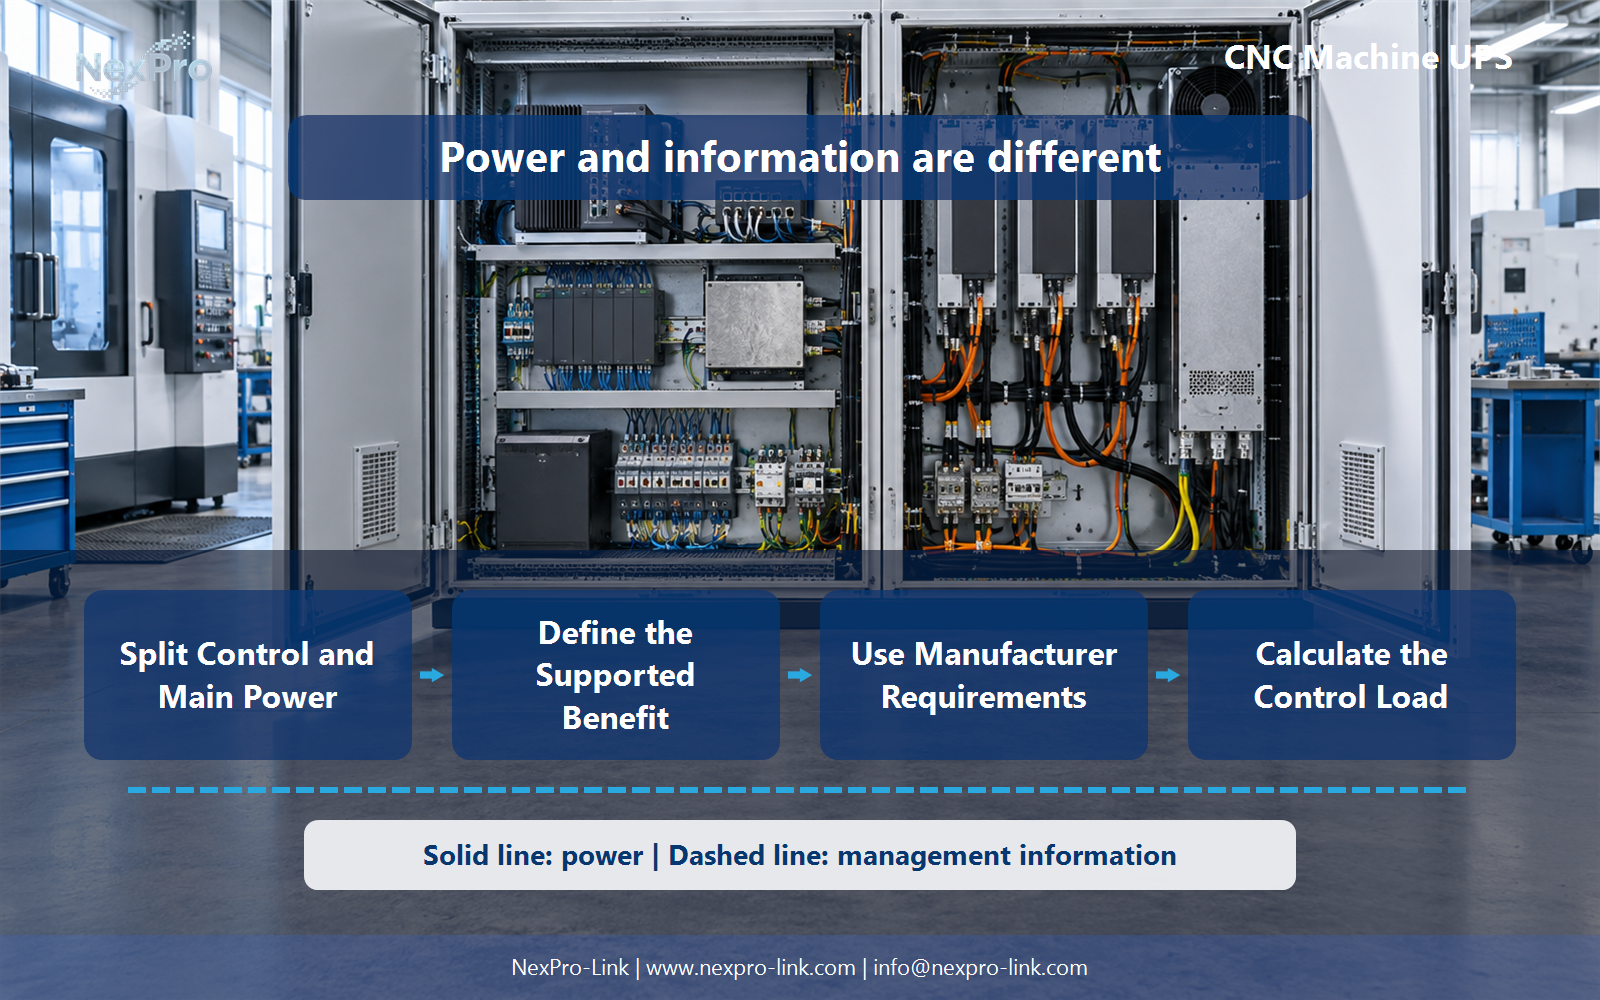
!The functional relationships behind CNC UPS controller spindle power difference; power delivery and management information are shown separately.
Section 03
Use Manufacturer Requirements
Selection should follow the CNC manufacturer's specified inputs, source behavior and approved backup interfaces. A nominal wattage comparison is not enough for a mixed machine load. The control cabinet may include a single-phase supply, a 24 V DC rail, or both, and the transition behavior matters as much as the steady rating.
Keep any dedicated control or drive backup equipment distinct from a general IT UPS. An office UPS sized for a workstation is not automatically the right box for a machine tool.
The interface schedule turns a data-sheet comparison into a checklist. If the manufacturer names a preferred backup interface, use it. If the manual is silent, ask for the supported shutdown behavior before finalizing the equipment.
- Confirm the answer to: Which power requirements should guide selection?
- Draw electrical power as a solid path and management information as a separate dashed path.
- Keep external services and specialist approvals outside the UPS equipment claim.
Section 04
Calculate the Control Load
Size the control-only UPS from the devices required for the stop or data-preservation sequence. Include the relevant peaks and any source conversions at one consistent boundary. The interval should follow that sequence. Do not set it from a guess about how long machining could continue.
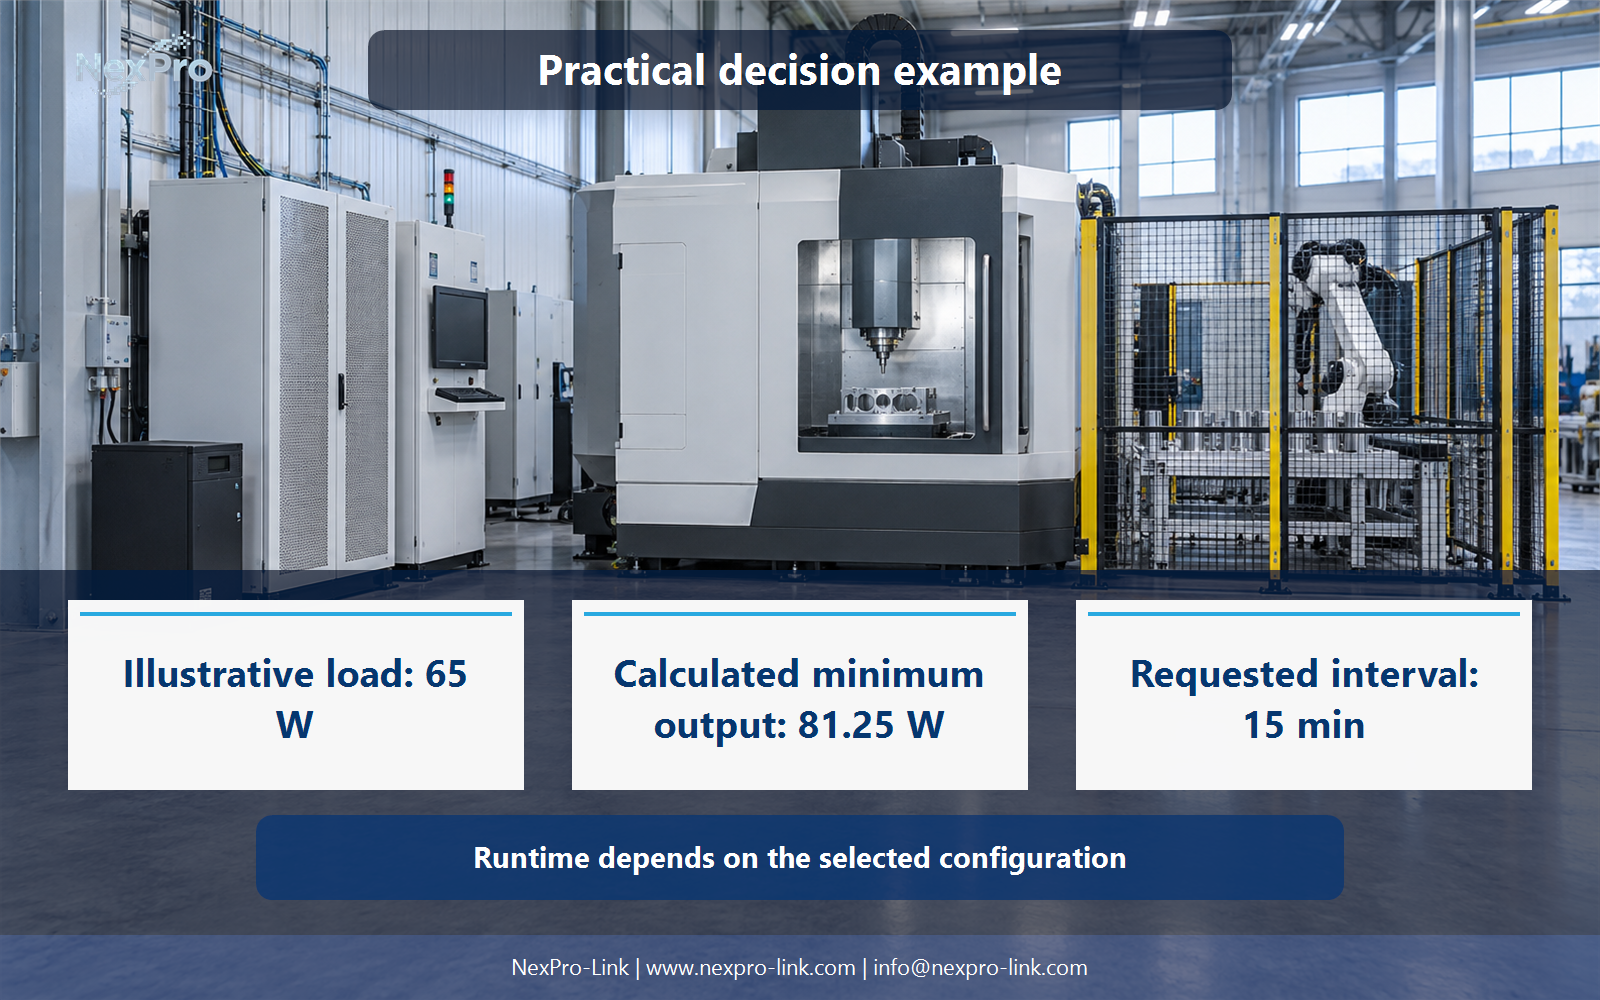
The numbers below are an illustrative example. They are teaching inputs, not a measured installation.
Total protected AC input comes to 65 W. Two limits follow from that total. Apparent power uses the assumed aggregate power factor, and a utilization ceiling keeps the converter from running at its edge.
The W and VA minimums are checked separately because they rarely cross the same part of a converter's curve. The 16.25 Wh figure is load-side energy, before conversion losses, discharge rate, temperature and ageing. It is not a battery purchase number, and it is not a runtime guarantee.
Section 05
Plan Restart Authority
Should the CNC restart automatically after utility recovery? Only through the machine's approved procedures and required operator checks. Confirm the control state and process conditions before production resumes.
Automatic restart is tempting because it looks faster. On a machine tool it can be the wrong default. A spindle that spins back up with a tool still in the cut, or with offsets unconfirmed, creates a hazard the control backup was never meant to manage. Write the recovery map for the project and keep supply, controls, machine checks and the operator in the same record.
The recovery map keeps the equipment inputs and the intended service outcome aligned. It also gives the operator one page to follow on the day the power comes back, when the shift is already under pressure.
Section 06
Prepare the Machine-Specific RFQ
At this point the analysis turns into a supplier brief. Provide the machine's approved backup scope, electrical requirements and intended control response. NexPro-Link can discuss equipment matching for that boundary. Whole-machine compatibility, drive behavior and safety functions remain with the machine and integration teams.
Moving to a real quotation needs the UPS power catalog for equipment and the BOQ and tender support page when a load schedule is ready.
Engineering references
These sources support the general planning principles. Always use the selected product's current datasheet and applicable project standards for final design.